
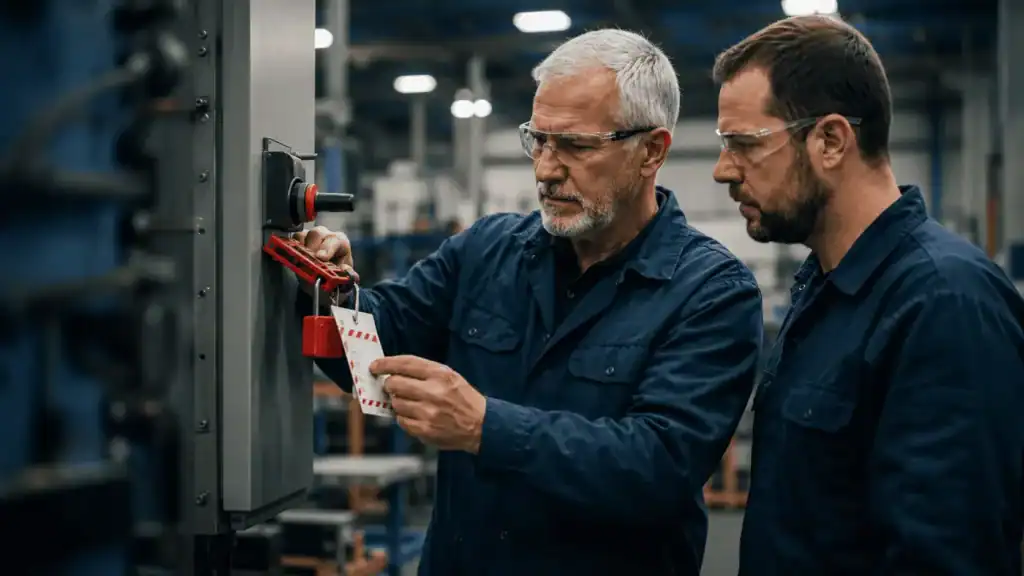
A maintenance worker climbs onto a press one Sunday morning to clear a jam. The machine looks dead. He decides not to apply his lock because “it will only take two minutes.” Meanwhile, a co-worker at the control panel restarts the cycle. This is exactly the kind of scenario the CNESST lockout-tagout procedure exists to prevent. And yet, year after year, the same mistakes keep showing up on the plant floor.
Key takeaways
- According to the CNESST, nearly 1,000 work accidents a year in Quebec (2010-2014) were caused by the unexpected release of energy.
- The RSST (sections 195 to 207 (formerly 188.1 to 188.13)) requires single-key locks, an energy inventory and a procedure specific to each machine.
- Most mistakes aren’t about hardware: they come from what people know, apply and can prove.
In this article
- What the CNESST lockout-tagout procedure really requires
- Mistake 1: forgetting an energy source
- Mistake 2: not verifying the absence of energy before starting
- Mistake 3: sharing locks or keys
- Mistake 4: mishandling the shift change
- Mistake 5: treating the contractor like a visitor
- Mistake 6: relying on a generic or non-existent procedure
- Mistake 7: train once, then forget
- The common root of these seven mistakes
In Quebec, between 2010 and 2014, there were an average of nearly 1,000 workplace accidents per year, including roughly four deaths, caused by the unexpected release of an energy source during installation, maintenance, repair or clearing work. These figures come from the CNESST. They are not cases of bad luck. They are almost always known, repeated gaps that a solid program would have caught.
Here are the seven lockout-tagout mistakes we see most often in industrial companies, and what the regulations actually require for each one.
What the CNESST lockout-tagout procedure really requires
Before talking about the mistakes, we need to set the context. Since the start of 2016, the Regulation respecting occupational health and safety (RSST) governs the control of hazardous energy in sections 195 to 207. A CNESST lockout-tagout procedure relies on an energy-control method that consists of applying a single-key lock to an energy-isolating device.
The basic rule is simple: as soon as someone has to enter the danger zone of a machine for work that is not routine production (installation, servicing, adjustment, inspection, unjamming, cleaning, repair, modification), lockout-tagout must be applied, or another method offering equivalent safety must be used. The word “equivalent” matters. It is not a loophole for improvising.
The employer must also keep an inventory of its equipment and their energy sources, produce machine-specific procedures, and ensure that anyone entering the danger zone has been trained and informed. It is these obligations that the following seven mistakes betray, one after another.
Mistake 1: forgetting an energy source
When people think “cut the power,” they think electricity. But an industrial machine often stores several types of energy at the same time. A hydraulic accumulator stays under pressure after shutdown. A pneumatic cylinder holds compressed air. A counterweight or a raised part can drop under gravity. A compressed spring can release without warning.
Section 201 of the RSST is clear on this point: the lockout-tagout sequence must include the elimination or, if that is impossible, the control of any residual or stored energy. Opening the main disconnect switch is almost never enough. The root cause of this mistake is almost always the lack of a complete inventory of energy sources for each machine. Without that mapping, even the most conscientious worker in the world will miss one.
Mistake 2: not verifying the absence of energy before starting
Applying your lock is one thing. Confirming that the machine is truly neutralized is another. Too many people skip the verification step because they take isolation for granted.
The regulations call for tests: attempting to start the equipment from the control panel to confirm it does not restart, and verifying with the appropriate instruments that the sources are indeed inactive. A disconnect switch can be faulty. A wire can be mislabelled. A valve can leak. The rule of the trade fits in one sentence: never trust a switch, confirm the absence of energy with an instrument before you put your hands in the machine.
Mistake 3: sharing locks or keys
The lockout-tagout lock must be single-key. That means one key, one person. The fundamental principle of energy control is that the machine cannot be restarted without the deliberate action of every person who has access to the danger zone.
The moment a supervisor keeps a master key “just in case,” or a crew shares a common lock with duplicate keys, the whole system falls apart. When several workers are involved on the same machine, each one must apply their own personal lock, often on a hasp or a lockout box. No one restarts until the last lock is removed by its owner. It is mechanical, it is physical, and it is what makes the system reliable.
Mistake 4: mishandling the shift change
Here is a classic from the evening shift. A worker finishes their shift in the middle of a repair. They remove their lock, leave, and the relief will arrive “soon.” In between, the machine is no longer protected by anyone.
The written procedure must provide continuity measures for these exact situations: shift changes, waiting for parts, staff rotation. The worker who is leaving must wait until their replacement has applied their own lock before removing theirs. And before leaving, they must pass on all relevant information about the status of the work. That handover between two shifts, when it is not structured, is one of the most dangerous holes in a lockout-tagout program.
Mistake 5: treating the contractor like a visitor
The technician from the outside firm who comes to repair the conveyor does not know your plant. He does not know your disconnect switches, your isolation points, your quirks. Yet we regularly see him climb onto the equipment with his own gear and his own method, with no coordination with the establishment.
The employer with authority over the establishment must ensure that anyone with access to the danger zone of a machine, including outside personnel, is informed of the risks and the applicable energy-control measures. When several employers cross paths on the same equipment, coordinating the lockout-tagout becomes mandatory, not optional. A contractor who applies lockout-tagout “his own way” without connecting to your procedure is an accident waiting to happen.
Mistake 6: relying on a generic or non-existent procedure
Many plants have a “lockout-tagout program” that fits on a laminated sheet posted near the door: cut, lock, verify. It is better than nothing, but it does not meet the requirement. The regulations call for a procedure specific to each machine, one that identifies its energy sources, its isolation points, the equipment required and the precise steps to neutralize it.
A hydraulic press, an industrial furnace and a bottling line have nothing in common in their safe-shutdown sequence. A generic sheet forces the worker to improvise, and improvising in front of hazardous energy is precisely what the law seeks to eliminate. Building these sheets forces you to put down in black and white, machine by machine, what only a few veterans carry in their heads, a step that the CNESST lockout-tagout procedure makes unavoidable. On that front, mapping critical knowledge becomes a valuable tool for leaving nothing in the blind spot.
Mistake 7: train once, then forget
The seventh mistake is the most insidious because it cannot be seen. A company rolls out its procedures, trains everyone once and for all, checks the box, and moves on. Three years later, half the team has changed, the newcomers learned “on the job” by watching an older worker, and no one can prove who was trained on what.
But the obligation to train and inform workers is not a one-time event, it is a permanent state. Every new employee, every assignment to a new machine, every equipment modification resets the counter. In the event of an inspection or, worse, an accident, the employer must be able to demonstrate that the exposed person had received the required training and information. Rigorous tracking that shows who was trained on which procedure, and when, makes all the difference on the day of an inspector’s visit. That is exactly what you get with an training-tracking tool built for SMEs.
The common root of these seven mistakes
Look at them again. The forgotten energy source, the botched shift change, the contractor left to his own devices, the training that evaporates: in almost every case, the physical lock is not the problem. The problem is what people know, what they apply and what they are able to demonstrate.
Lockout-tagout is not just a matter of hardware. It is knowledge that must be documented, taught and kept up to date over time, in the same way as structuring mentorship or onboarding new employees during a labour shortage. A perfect CNESST lockout-tagout procedure that lives only in a veteran’s head protects no one the day he is not there.
That is why the first concrete step for many plants is not to buy more locks. It is to make sure everyone understands what the control of hazardous energy is and why every step of the CNESST lockout-tagout procedure matters. Witeach offers exactly that, a free lockout-tagout awareness course in its catalogue, a no-commitment entry point to get your team aligned on the same basic reflexes before going further.
📚 Read next
Do you recognize your operation in one or more of these mistakes? That is already a good starting point. Begin with the free lockout-tagout awareness course, then book your free self-assessment to see where your blind spots are. We look at it together, no pressure.
